The food manufacturing and processing sector is no stranger to disruption, but recent years have tested even the most robust operations. Global instability, logistics bottlenecks and changing trade requirements have placed pressure on manufacturers to maintain production, keep shelves stocked and fulfil customer contracts.
Geopolitical events, including the war in Ukraine, have contributed to volatility in the availability and cost of some raw materials, as well as energy and transport, while disruption to key shipping routes has led to longer journeys and increased freight costs. Reduced road haulage capacity and HGV driver shortages have added further pressure on the movement of goods, while changes to trade tariffs and the continuing effects of Brexit have made international sourcing more complex.
For food manufacturers and processors, the combined effect has been longer lead times, less predictable deliveries, rising input costs, and shortages of key ingredients.
Considering contingencies
When a critical ingredient becomes unavailable, food manufacturers and processors have several options – try to source it from another supplier, qualify an alternative ingredient, draw on available stock, or adjust production schedules while waiting for the original supply to arrive.
Each option has its own advantages and limitations: holding additional inventory can provide a buffer against delivery delays but ties up working capital and requires suitable storage; developing relationships with more than one supplier reduces dependence on a single source but requires extensive assessment to ensure quality and technical requirements can be met; and changing a formulation may help keep production moving, but only if the substitute is suitable for the product and can be incorporated safely into the manufacturing process.
Where production capacity is the problem, transferring work to another facility or using a third-party processor may also be worth considering.
When supply is disrupted, procurement teams may understandably focus on finding a replacement that meets the required product specification. However, two ingredients that appear equivalent on paper may behave differently during processing.
Differences in composition, concentration or impurity levels can affect how ingredients interact with one another and with production equipment. Processing requirements can also vary. For example, two materials intended for the same mixing operation may need different temperatures or heating times to achieve the required consistency. A substitute that needs to be heated for longer, or to a different temperature, could mean changing established operating procedures.
These differences can have a significant impact on production processes designed around particular material characteristics and operating conditions. Changing an ingredient or supplier may therefore require adjustments to equipment settings, handling arrangements or quality checks. Manufacturers and processors need to assess whether an alternative is suitable for both the finished product and the process used to make it.
The same applies when moving production to another facility. Even if the ingredients and finished product remain unchanged, differences in equipment, plant layout, storage and processing arrangements can affect how the operation is managed.
Changes should be properly assessed and documented before production moves ahead. Existing procedures and safeguards should not simply be assumed to remain suitable because the replacement ingredient or facility appears similar to the original.
Could toll processing help?
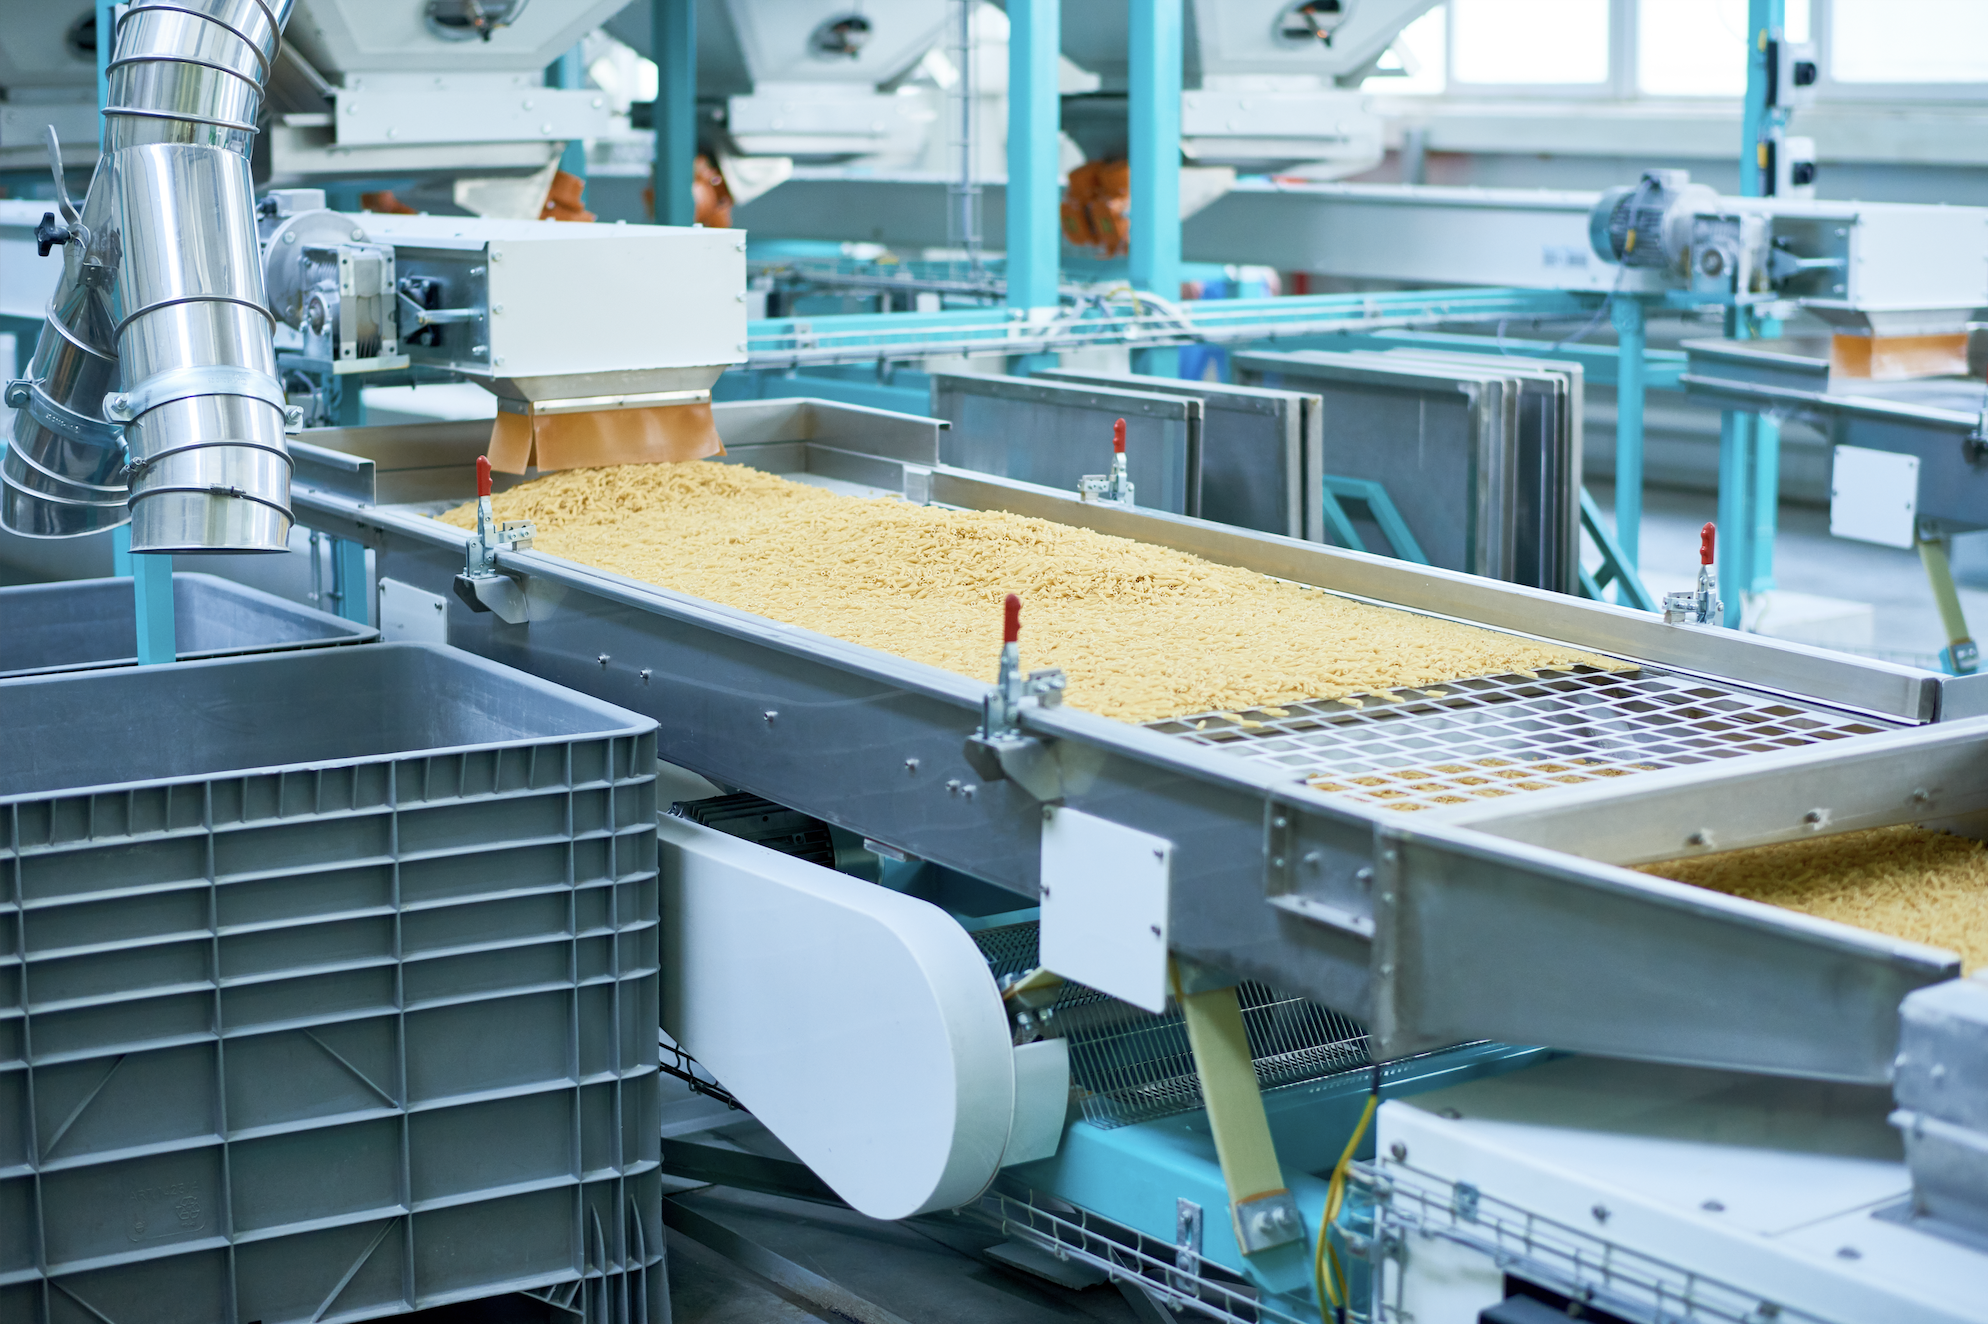
One option for food sector businesses facing supply disruption or capacity constraints is to work with an experienced toll processor, which allows them to use an external facility and workforce to carry out specified production operations.
This can provide access to additional processing capacity without the lead time and capital investment involved in expanding an existing plant or building new infrastructure. Depending on the provider’s capabilities, it may include kibbling, powder and liquid blending, custom formulations and multi-ingredient blending.
Toll processors can also offer technical resources that may not be readily available in-house, such as specialist equipment, quality testing and laboratory services to support product checks and batch release. Some providers can also support pilot trials, formulation optimisation and new product introductions.
Established supplier and logistics networks offer another potential advantage. Toll processors may have access to surplus stock and alternative raw material sources, helping manufacturers locate hard-to-source ingredients.
Additional services, including warehousing, transport, import and export support, labelling, packing and repacking, can help address other points of vulnerability in the supply chain.
Keeping options open
While working with a toll processor offers several benefits, it is not a universal solution. Importantly, outsourcing does not remove responsibility for product quality, safety or compliance.
Before outsourcing, food manufacturers and processors should establish whether a potential partner has the appropriate equipment, technical knowledge and quality management systems, as well as suitable arrangements for storing, handling, processing and transporting ingredients.
Relevant food-sector accreditations, sampling and analysis procedures, batch traceability and supporting documentation should also form part of the assessment.
It is equally important to consider practical issues such as lead times, logistics, available capacity and how the external operation will fit into existing production and distribution arrangements. A provider’s supplier network and range of additional services may be valuable, but these should be assessed against actual requirements.
More broadly, food manufacturers and processors should avoid becoming dependent on a single contingency route. A toll processor may provide useful additional capacity, but it should sit alongside other strategies, such as alternative suppliers, appropriate stockholding and the ability to adjust production schedules.
Planning ahead
Effective contingency planning is not simply about finding a replacement when supply fails. It starts with identifying the materials, suppliers and facilities on which production depends, then assessing where an interruption would have the greatest impact.
Food manufacturers and processors can use this process to identify alternative suppliers, investigate suitable substitute ingredients, review stockholding arrangements and assess whether production could be transferred to another facility.
Potential toll processing partners can also be identified and assessed before their services are urgently needed.
Crucially, alternatives should be considered in advance for their technical suitability, quality implications and regulatory requirements. This does not remove the need for a formal review when a change is implemented: the actual ingredient, supplier or facility must still be verified, and any necessary adjustments to procedures and controls made.
Planning also needs to reflect commercial realities. Additional inventory, alternative supplier arrangements and external processing capacity all have costs, which must be weighed against the potential consequences of production interruption.
Supply chain disruption is unlikely to disappear, and no single measure can protect food-sector businesses from every eventuality. By identifying vulnerabilities and assessing alternative suppliers, materials and processing arrangements in advance, businesses can respond more quickly when disruption occurs while protecting production, product quality, and customer commitments.
Forbeats is a chemical management, processing and consultancy company that offers a range of materials handling and management services. Its end-to-end service options include powder and liquid blending and packing, logistics, distribution, storage and import/export services to a range of leading markets, including the food and beverage sector.
Ben Beattie, director of Forbeats, is a toll processing and contract manufacturing specialist with experience in the chemical, food and pharmaceutical sectors. He provides practical insight into process optimisation, production management and the technical and commercial considerations involved in outsourcing manufacturing operations. His expertise includes helping businesses assess external processing options, manage operational risks and maintain quality and safety standards.